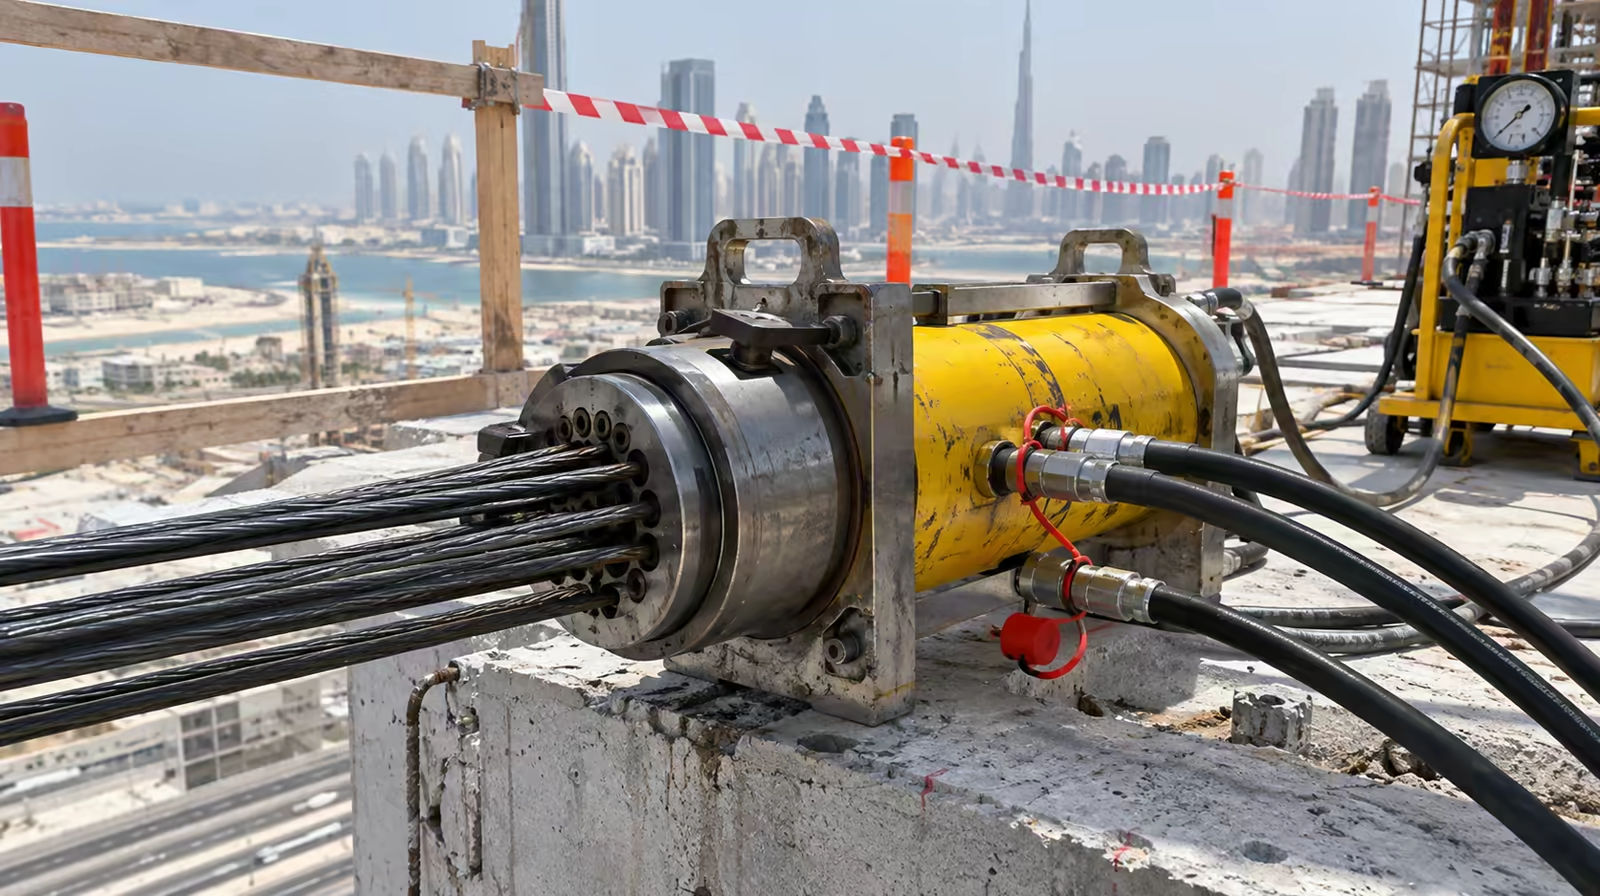
Stressing takes a fraction of the time the rest of the work takes, it is the point of highest stored energy on the site, and it is the operation that turns the design into a structure. On stressing operations we carry out across the UAE, the sequence below is what happens at the jack and why the numbers matter.
What Has to Be True Before Stressing Can Begin?
The concrete has reached the specified strength. This is not negotiable and it is not a matter of days elapsed. The anchorages transfer enormous force into a small area of concrete, and concrete that has not reached the required strength will crush locally under the anchorage. The strength is confirmed by testing cubes cast from the same pour and cured alongside the slab, not by the calendar.
This matters more in the UAE than in cooler climates, and in both directions. High ambient temperatures accelerate early strength gain, which can mean a slab is ready to stress sooner than a programme assumed. But the same heat drives rapid moisture loss, and concrete that has dried out rather than cured does not reach the strength the curve predicts. Neither outcome is knowable without testing cubes that were cured in the same conditions as the deck.
Formwork conditions are right. The slab has to be able to shorten. A post-tensioned floor gets slightly shorter as the prestress is applied, and formwork or props restraining that movement will fight the prestress. What can be struck before stressing and what must stay is specified, not improvised.
Access is available at every live end. The jack needs physical room. An anchorage that cannot be reached cannot be stressed, and by this stage there is no fixing that cheaply.
The stressing sequence is agreed. Tendons are not stressed in an arbitrary order. The sequence controls how the prestress builds across the slab and keeps the structure from being loaded unevenly during the operation.
What Happens at the Jack?
The strand is gripped by a hydraulic jack at the live end and pulled to a specified force.
Two numbers are recorded for every tendon. The pressure on the jack, which corresponds to the force being applied. And the elongation, which is how far the strand has actually stretched, measured physically.
When the target force is reached, the jack is released. Wedges in the anchorage bite into the strand and hold it, locking the force into the tendon. A small amount of movement occurs as the wedges seat, which is a known and calculated quantity rather than a loss of quality, and the design accounts for it.
The tail of strand protruding beyond the anchorage is then cut off, and the anchorage pocket is sealed. In a bonded system, grouting follows.
Why elongation is the number that matters
Force alone does not prove anything.
Take a tendon that is obstructed somewhere along its length, perhaps a duct crushed during the pour or a tendon fouled on reinforcement. The jack will still reach the target pressure, because it is pulling against a resistance. But the strand beyond the obstruction is not being stretched, so the force is not distributed along the tendon as designed. The pressure gauge says the operation succeeded. The tendon is not doing its job.
Elongation catches this. If a tendon stretches materially less than calculated, force is not reaching where it should. If it stretches materially more, something else is wrong, possibly a strand slipping or an anchorage not holding.
Every tendon has a calculated elongation derived from its length, profile, and the friction expected along it. The measured figure is compared against that calculation, and each has to agree within tolerance.
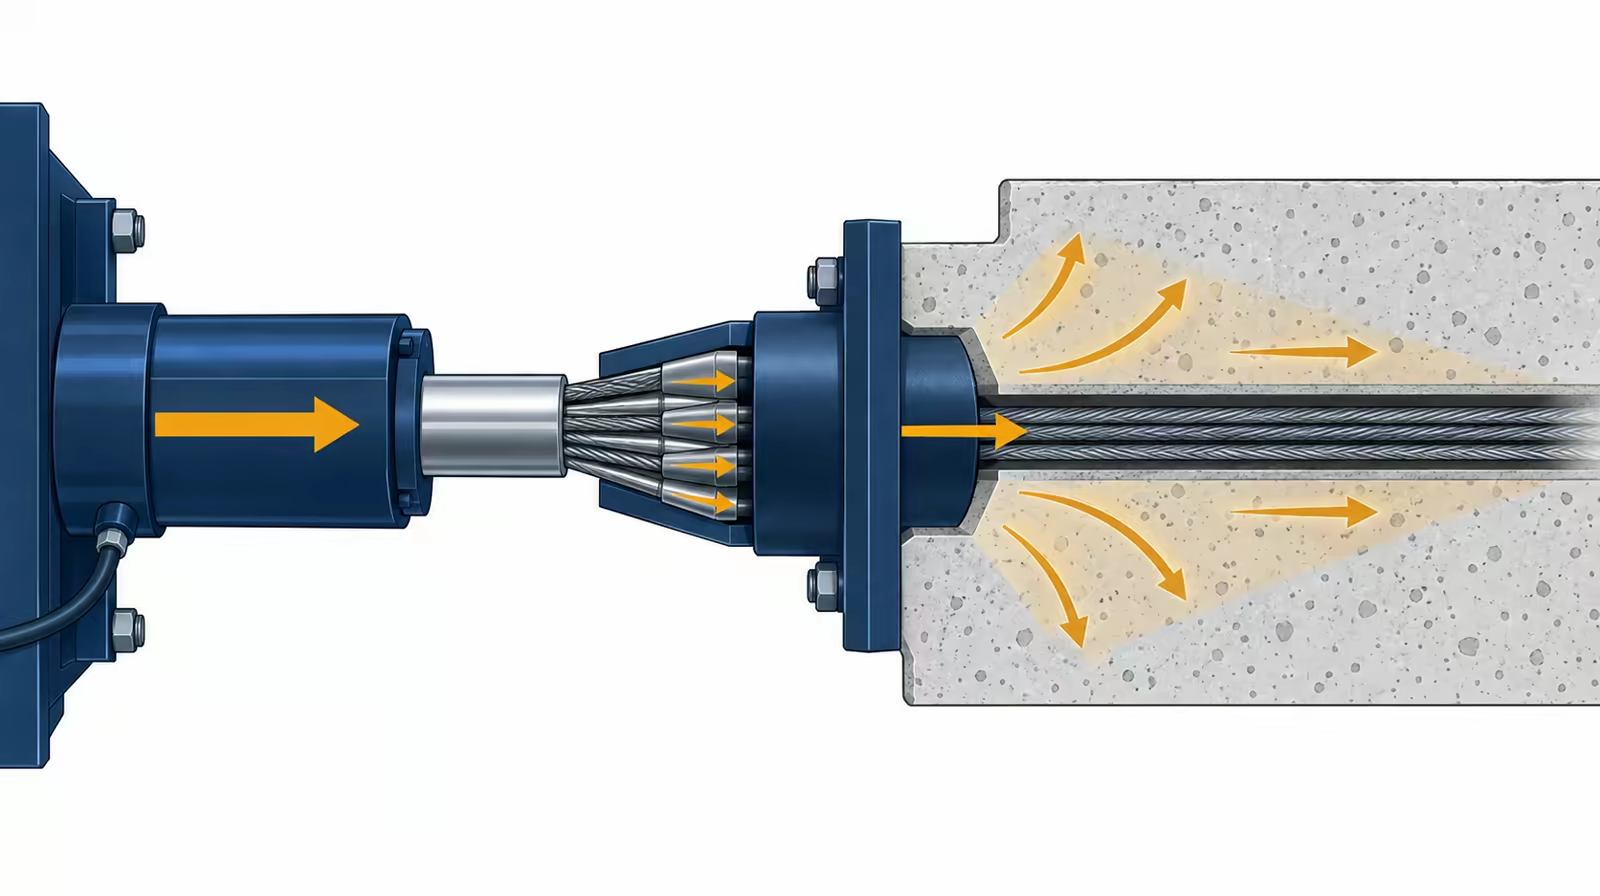
Pressure at the jack and measured elongation along the strand: two independent readings that have to agree.
What Happens When a Reading Falls Outside Tolerance?
It is investigated before anyone moves on. That is the entire value of measuring.
The usual causes are identifiable: friction higher than assumed because a duct deviated from its intended profile, an obstruction in the duct, a wedge that has not seated properly, or a calculation input that did not match what was built.
The remedies depend on the cause. Sometimes a tendon can be stressed from the opposite end, which redistributes the friction and often resolves the reading. Sometimes the tendon has to be investigated physically. Occasionally the design is revisited to confirm the slab is still satisfactory with the force actually achieved, which is a legitimate engineering answer rather than an admission of failure.
What must not happen is the reading being accepted because the pressure gauge looked right. An out-of-tolerance elongation is information about the structure, and ignoring it means building on top of an unknown.
Who Should Be Watching, and What Do They Receive?
Stressing is normally a hold point. The consultant or their representative witnesses it, because it is one of the few operations on a concrete frame where the quality of the work is directly measurable while it happens rather than inferred afterwards.
What they receive is a stressing record: every tendon identified, the force applied, the calculated elongation, the measured elongation, the variance, and the concrete strength the operation was carried out at. That record goes into the project documentation, verified through inspection and testing, and is what releases the next stage of work.
It is also the document that matters most in ten years. If a question ever arises about a floor, the stressing record is the evidence of what was actually achieved, tendon by tendon.
Across our projects in Ajman and elsewhere in the UAE, the stressing scope is contracted alongside design, installation and grouting rather than separately, and the elongation record is produced for the consultant as a matter of course rather than on request. Cube testing to confirm concrete strength before stressing is part of the same scope.
See how this plays out across our post-tensioning work across the UAE.